HMI v priemysle | Ako má vyzerať moderný Human-Machine Interface? | HMI in Industry | What Should a Modern Human-Machine Interface Look Like?

HMI in Industry | What Should a Modern Human-Machine Interface Look Like?

If you manage production, you probably have access to more data today than ever before. Even so, a simple problem can arise at a critical moment. An operator, technician, or shift supervisor may not be able to understand quickly enough what is happening, where the problem occurred, and what the next step should be. If a screen displays dozens of colors, values, and icons without a clear priority, people cannot quickly distinguish between a normal state, a warning, and a truly critical condition. And if the interface does not help them do so, the HMI becomes another source of cognitive load.

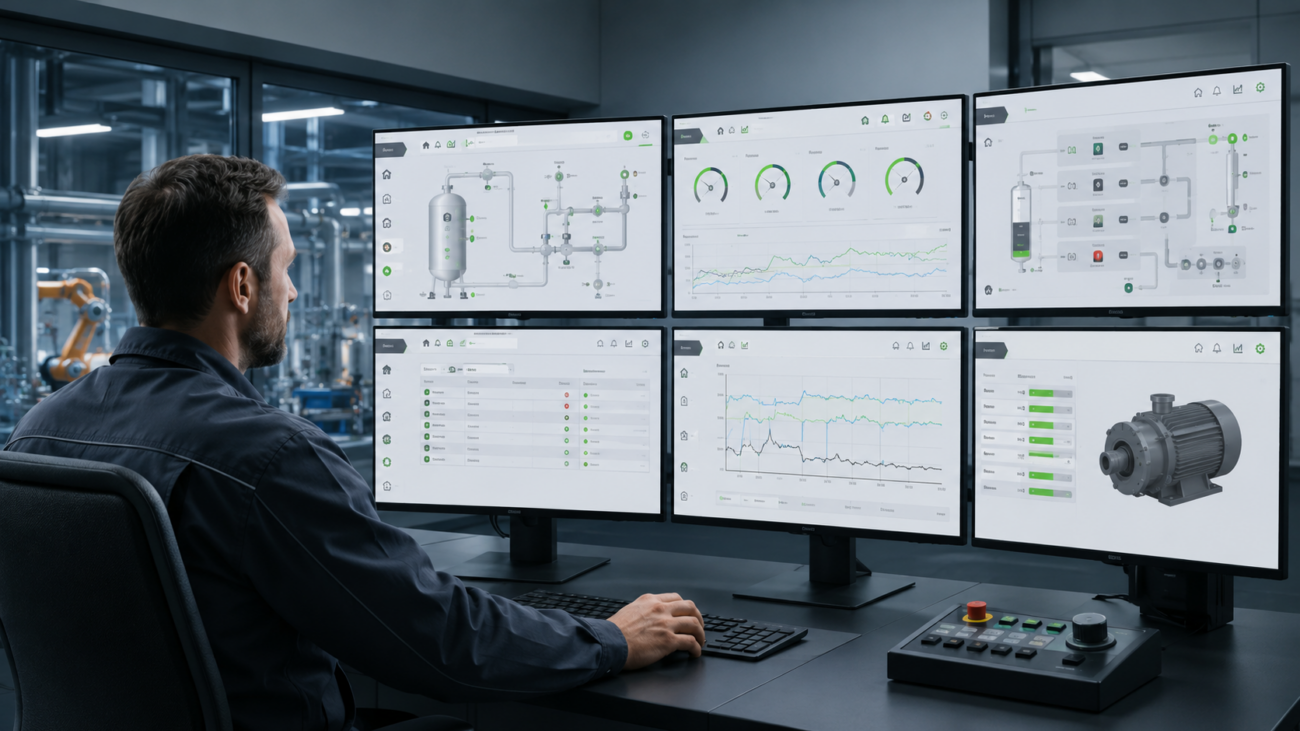
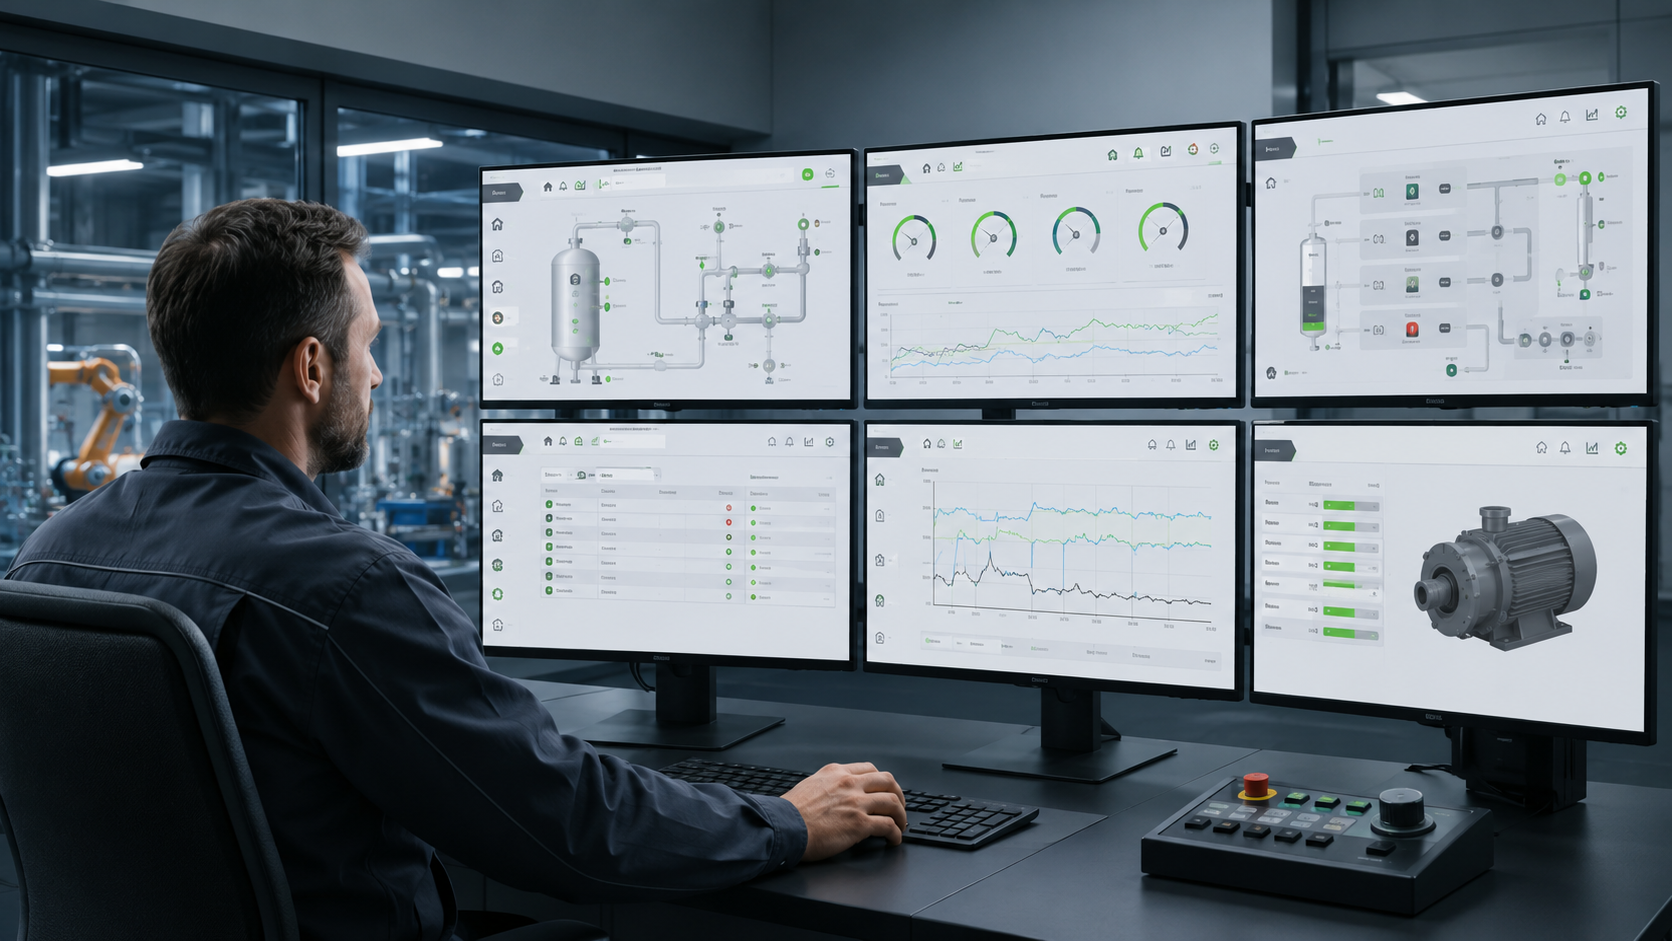
That is precisely why HMI (Human-Machine Interface) is one of the most important layers of modern industrial automation. Modern HMI design should not primarily be visually appealing. It should be clear, safe, consistent, and designed around how people work in real-world operations. A well-designed HMI helps operators respond more quickly, maintenance personnel identify the causes of problems more efficiently, management better understand production, and the company reduce the risk of errors, downtime, and inefficient interventions.
HMI v priemysle | Ako má vyzerať moderný Human-Machine Interface? | HMI in Industry | What Should a Modern Human-Machine Interface Look Like?

Human-Machine Interface – DEFINITION

What does HMI (Human-Machine Interface) mean?

The definition of 💡 Human-Machine Interface is essentially simple. HMI is a user interface through which a person communicates with a machine, production line or the entire process. The main significance of HMI lies in the fact that it turns raw data into usable information. In practice, HMI enables users to monitor operating values, control equipment, change permitted parameters, acknowledge alarms or analyze trends. A good HMI is therefore a critical point of interaction between a person and the system.

Why does HMI fail even when the technology works correctly?

❌ In many companies, digital transformation places the greatest emphasis on hardware, data collection, and architecture, as well as various integrations. This is understandable because without a reliable technical layer, the system cannot function. The problem arises when the user interface is addressed only at the end of the project as a visual output that is supposed to “somehow display the data.” The result is then an HMI that is technically correct but operationally weak.

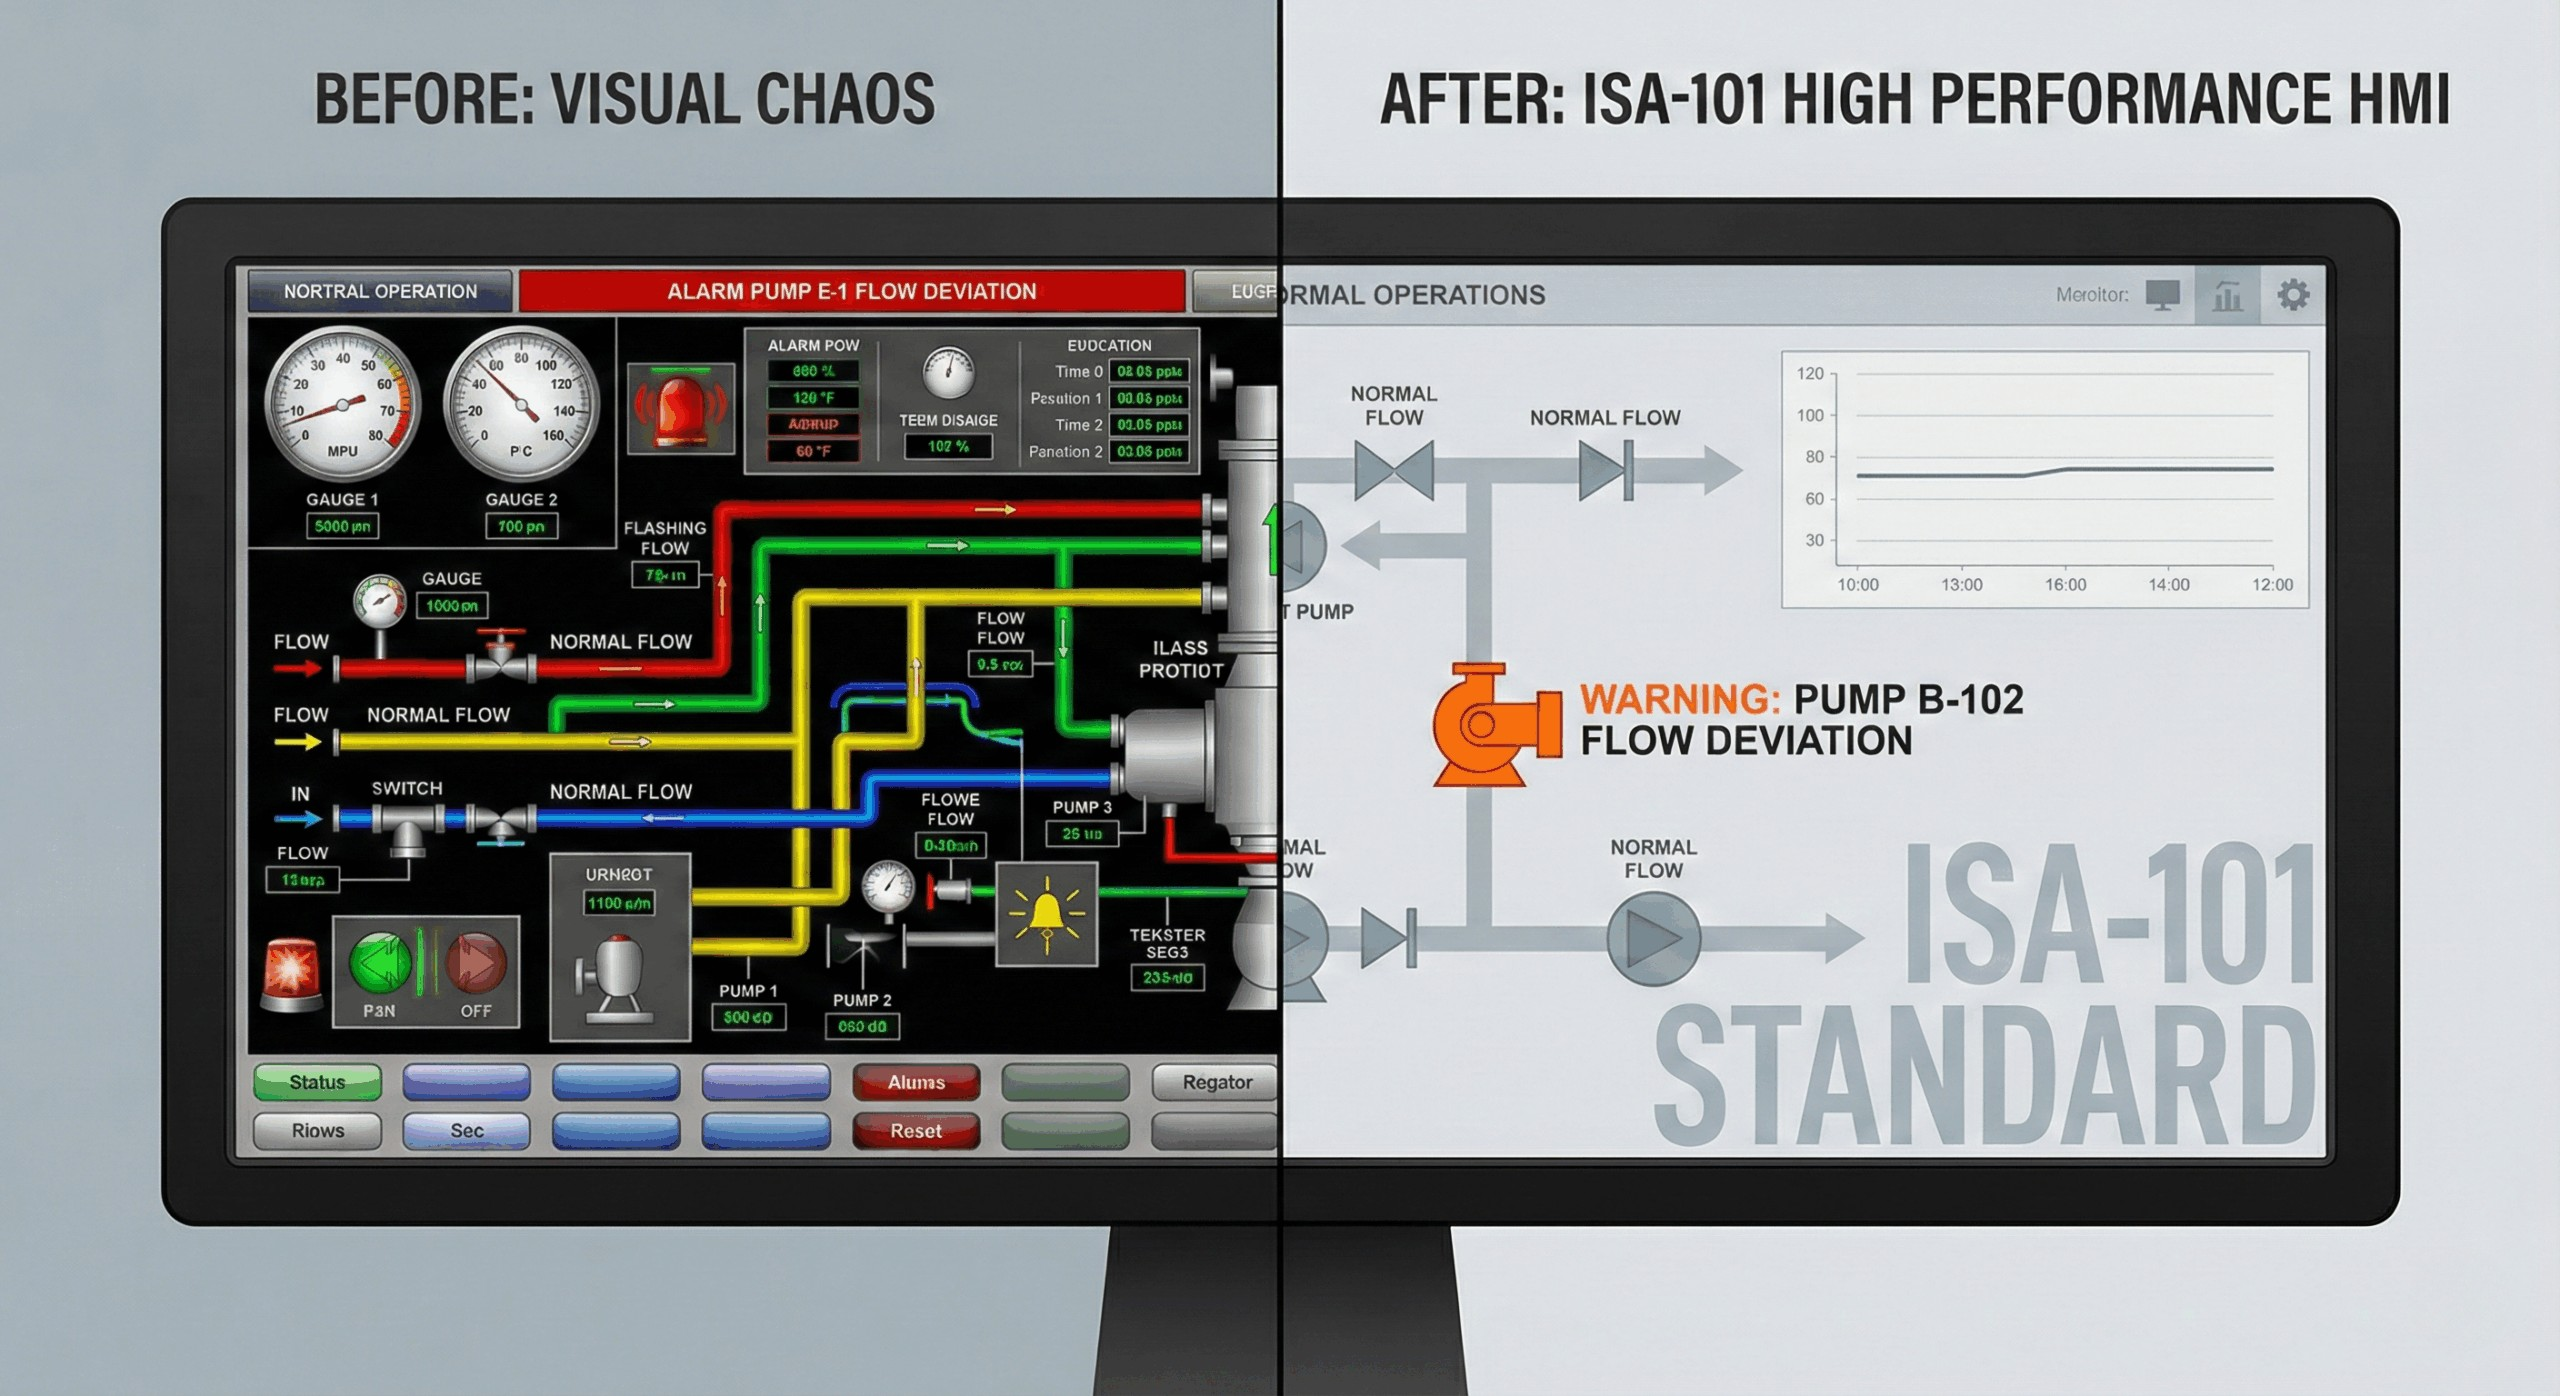
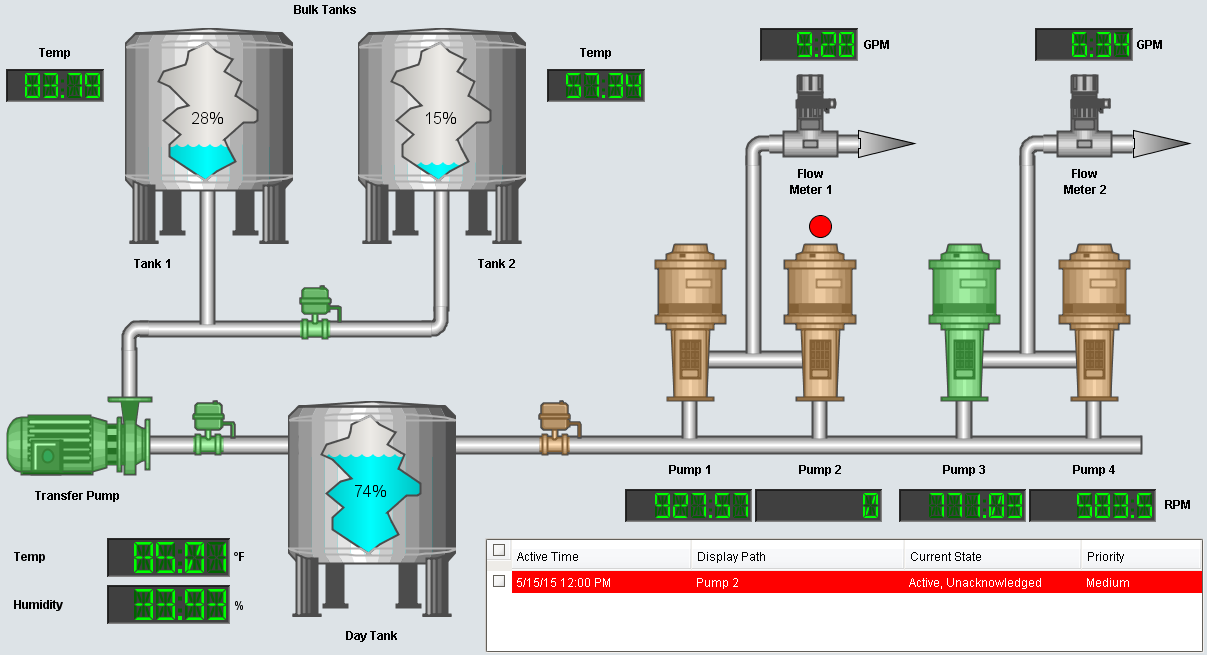
❌ Screens often copy process schematics, contain too many details, and use many colors, animations, and icons, while all elements have similar visual importance. The operator then cannot clearly see what is merely a normal part of the process and what genuinely requires attention. During a fault, they even have to switch between multiple views to piece together a picture of the situation. Inconsistency is also a common problem. One screen uses red for an alarm, while another uses it for an important parameter.

❌ This situation arises mainly because HMI is designed from the technology’s perspective, not the user’s perspective. The designer knows how the line works, where the equipment is located, and what the individual values mean. However, at a particular moment, the operator needs answers to more practical questions: Is the process within normal limits? Where did the deviation occur? What is causing it? What action is required? And what will happen if I do nothing? If HMI does not answer these questions quickly and clearly, it fails to fulfill its main role.

Most common risks of poor HMI

⚠️ The first risk is a slower response to faults and deviations. If the operator cannot see which parameter has moved outside the normal range, how long the problem has lasted, and which part of the production system is causing it, they lose time looking for connections. Instead of taking immediate action, they analyze the screen, switch between views and verify information with colleagues. In practice, even a short delay can mean longer downtime, higher costs and a greater risk that a minor deviation will become a more serious operational problem.

⚠️ The second risk is incorrect interventions. If the system does not display clear alarm priorities, the user may respond to a less important problem and overlook a critical condition. The problem is even greater when the HMI generates too many alarms. Operators get used to them, start acknowledging them automatically and the alarm stops being a signal that requires attention. This phenomenon is so common that it is known as alarm fatigue, or fatigue caused by alarms.

⚠️ The third risk is lower work efficiency. If a simple operation requires an unnecessarily high number of clicks, if data has to be transcribed manually or if the user cannot quickly find the information they need, the system slows down work instead of speeding it up. In practice, this may mean, for example, that the operator spends more time operating the system than actually resolving the situation in production. With repetitive tasks, these small time losses gradually add up and can represent significant inefficiency.

⚠️ The fourth risk is dependence on experienced individuals. In companies with weak HMI, it is often the case that an experienced operator “knows where to look for things”, but a new employee gets lost in the system. This extends training, increases the risk of errors and makes work standardization more difficult. The problem becomes most apparent during staff changes or holidays or in crisis situations, when an experienced employee is not currently available. A quality HMI should ensure that the correct procedure does not depend solely on a specific operator.

⚠️ The fifth risk is poorer scalability of the entire system. If each screen is created without uniform rules, each new technology introduces its own control logic, different colors, different navigation and a different way of displaying information. This complicates system expansion, increases maintenance costs and means that instead of a unified digital environment, a collection of inconsistent screens emerges. At a larger scale, every modification or extension becomes unnecessarily more difficult than it would be with a unified HMI standard.

HMI Design Standards

HMI design standards have a highly practical significance in industry. They ensure that the interface does not depend on personal taste of a particular designer, but on uniform rules that can be used throughout the entire plant. HMI guidelines should therefore define how colors, typography, symbols, and navigation are used… If a company has multiple lines, production halls, or facilities, a unified HMI standard significantly simplifies the work of operators, maintenance teams, and internal technical teams.

When designing a modern HMI, the ISA-101 standard is often used as a basis. It helps establish rules for how HMI screens should be designed, used, and maintained over the long term. The aim is for the user to quickly understand what is happening and respond to abnormalities in time and for all screens to operate according to the same logic. The ISA-101 standard was even recently adopted as the international standard IEC 63303. This officially placed its principles among recognized standards used throughout industry worldwide.

Modern Human-Machine Interface Design

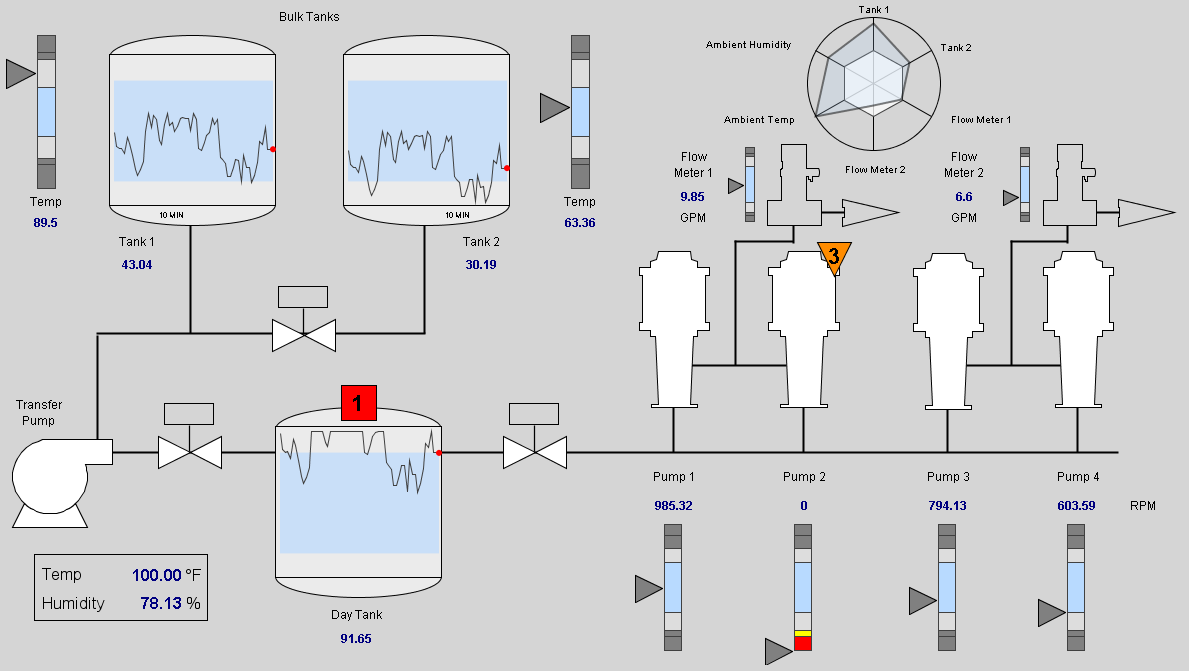
➡️ Modern Human-Machine Interface design no longer “displays everything”. It should display only essential information, and do so in a way that allows people to understand it quickly and correctly respond to it. In practice, this means that if everything is running correctly, temperatures are within normal limits, pressure is stable, and equipment is operating as expected, the screen does not need to be filled with bright colors, flashing elements, and animations. Quite the contrary. Normal operation should be displayed neutrally, so operators do not have to constantly evaluate every detail.

➡️ Visual emphasis should be reserved for deviations. This is where the use of colors plays an important role. Gray and neutral shades represent normal conditions. Yellow or orange indicates a warning, a deviation or a condition that requires attention. Red is reserved for critical situations in which an immediate response is required. As a result, every color has a clear meaning and the operator does not have to think about what a given visual element means.

➡️ Good HMI design, however, does not base the meaning of information solely on color. In practice, it is also necessary to consider that some users may have color vision deficiency. Therefore, critical states, alarms, and important warnings should be supplemented with unambiguous shapes, symbols or text labels. This allows the operator to distinguish important information even when they do not perceive colors in the same way as others. The result is an interface understandable to a wider range of users.

➡️ Also very important is the hierarchy of screens. High Performance HMI does not overwhelm the user with details on the home screen right away. First, it shows the overall state of the process. Next, it directs the user to the part where the problem occurred. Only then does it offer details of the specific device, a trend, diagnostics or service information. The user therefore does not have to search the entire system during a fault, but proceeds naturally from the general overview to the specific cause and solution.

➡️ No less important is displaying values in context. A number on its own often is not enough for the user, because it does not show whether the condition is still safe, approaching a limit or gradually deteriorating. A modern HMI should therefore also work with normal ranges, trends, and limits, so that the operator sees not only the current state, but also its progression. This enables the operator to better distinguish a short-term fluctuation from a problem that is gradually worsening. The operator can thus respond proactively, rather than only when a fault occurs.

Human-Machine Interface – EXAMPLE

What is the difference between a poor and a modern HMI?

Let us imagine, for example, a production line that has stopped. In a poor HMI, the operator sees a large process schematic, numerous icons, and several alarms at once. They have to manually determine whether the problem was caused by a safety stop, missing material, or a motor fault. A modern HMI design would handle the same situation differently. In a High Performance HMI, they first see that the line is stopped. The system then clearly indicates that the problem is in a specific part of the line. After opening the details, they discover that material is missing from the hopper and the equipment is therefore waiting.

This approach significantly reduces the operator’s cognitive load. The operator does not have to monitor everything continuously. The system alerts them to what is deviating from normal and at the same time logically guides them from the overall overview all the way to the specific cause of the problem. This is the main value of modern HMI design. It does not appear as an overcrowded screen full of data, but as a work tool that helps people act quickly and safely. The result is an interface that does not demand attention constantly, but only when it is genuinely needed.

Human-Machine Interface – SIGNIFICANCE

How does HMI affect costs, safety, and decision-making in manufacturing?

Human-Machine Interface has fundamental importance in industrial automation. The system itself may collect accurate data, machines may be reliably connected, and processes may be automated, but if the user does not understand what they see on the screen, the value of the entire solution is significantly reduced. A well-designed HMI interface is therefore not merely a matter of operator convenience. It has a direct impact on operational costs, production efficiency, safety, and data quality, as well as the company’s ability to make better decisions.

One of the greatest benefits of a high-quality HMI is faster response to faults, deviations, and abnormal conditions. The operator can more quickly understand whether the process is within normal limits, where the problem occurred, and what action is required. For the company, this means a shorter response time, less unnecessary downtime and lower costs caused by delayed intervention. HMI also helps maintenance personnel identify the cause of a problem more quickly and plan service interventions more efficiently.

A quality HMI also reduces the risk of incorrect interventions. If alarms are clearly prioritized, critical conditions are clearly differentiated and control elements are designed unambiguously, the user can make the right decision even under pressure. This is important especially during faults, operating mode changes or when working with critical equipment. The result is greater operational safety, a lower risk of equipment damage and more stable production quality.

A properly designed HMI also helps train new employees. If screens have a consistent logic, the same color coding and consistent navigation, a new operator can find their way around the system more quickly. Work can be standardized more easily across shifts, lines, or facilities. This reduces the risk of errors, shortens training time and helps maintain a more stable operating approach even when personnel changes.

From the perspective of supervisors and management, Human-Machine Interface is also significant because it improves the quality of operational information. If HMI clearly displays line performance, reasons for downtime, recurring alarms, trends or deviations from the plan, it becomes an important source of data for process improvement. Management can therefore make decisions based on actual production conditions, not merely according to delayed reports, subjective estimates or incomplete records.

Ultimately, a quality HMI delivers concrete results to the company:

✅ Faster responses and less downtime
✅ Lower risk of errors and greater safety
✅ Easier employee training
✅ Reduced operating costs
✅ More efficient production management

Human-Machine Interface – APPLICATIONS

Where does HMI connect with SCADA, MES, OEE, CMMS, EMS, BMS, and BI?

Human-Machine Interface applications today are not used only to control a single machine. In modern facilities, they are often part of a broader digital ecosystem that connects production, maintenance, energy management, and building management as well as management decision-making. An example of a platform in which such HMI applications can be created is Ignition. The advantage of this approach is that HMI can grow with the facility and gradually expand to include additional functions.

When connected to a SCADA system, Ignition can display the state of the process, real-time operating values, and alarms or trends. In combination with an MES system, it can add production context, such as the plan, the number of units produced or the reasons for downtime. A separate area is OEE, where HMI helps monitor equipment availability, performance, and quality so that the company can see where the greatest production losses occur and subsequently eliminate them.

When connected to a CMMS system, it can help maintenance handle faults and service interventions as well as planned maintenance. HMI applications are also relevant to EMS and BMS systems, where they help monitor energy consumption and control heating, cooling, lighting, ventilation systems and other technologies. Data from these areas can subsequently be further analyzed in BI tools, such as Power BI. The company thus gains not only an up-to-date overview of operations, but also a basis for long-term optimization.

How to Begin Modernization?

HMI modernization should not begin with selecting colors or redrawing icons. It should begin with an audit of the current state. Look at the screens that are used most frequently. Find out where operators lose time, which alarms recur, which values they have to look up manually, and where errors occur and which tasks are unnecessarily complicated. A Human-Machine Interface diagram is also helpful when designing a solution, as it shows how HMI fits into the overall technological and data environment.

Next, it makes sense to create or update an HMI standard. It should define rules for screen layout, colors, typography, and symbols as well as navigation. If this step is skipped, every new screen may look different and the company will simply create a more modern version of the original chaos. A good HMI standard also simplifies work when expanding the system further, because new screens are not created from scratch, but according to a clearly defined logic.

For larger facilities, it is advisable to start with a pilot project. Select one technology, process or production line where improving the HMI offers a clear benefit. Design a new concept, test it with users, adjust it based on feedback and only then extend it to other parts of the facility. It is also important to think about training. Operators need to know why the screen looks different, what the new rules mean and how the new system will help them in their work.

How Do We Help with HMI at IoT Industries?

At IoT Industries, we view HMI as part of the entire digital ecosystem, not as a standalone graphic screen. When designing a solution, we therefore also address data sources, architecture, integration with other systems and practical usability in operations. We help companies analyze existing screens, identify weak points, design an HMI standard, prepare prototypes of new screens, and implement the solution so that it makes sense to operators, maintenance teams, and management.

Thanks to our many years of experience, we can connect the world of operational technology with IT systems and create interfaces that not only display data, but help people use it in practice. If you want to find out whether your current HMI truly helps people in your operations, schedule a consultation with us. We will review your existing interfaces and identify opportunities for improvement and propose practical steps for turning HMI into a tool that delivers real value for your production.

Why Choose IoT/IIoT Implementation with IoT Industries?

Traditional companies typically specialize in OT (operational technologies, such as production lines and devices) or classic enterprise IT systems. However, we are able to connect both of these worlds. Our unique expertise in integrating OT and IT allows us to deliver innovative solutions in digital transformation, enhancing efficiency, reliability, and competitiveness for manufacturing companies.
Kľúčové trendy v Industry 4.0 – Čo očakávať v roku 2026? | Key Trends in Industry 4.0 – What to Expect in 2026?

Key Trends in Industry 4.0 – What to Expect in 2026?

If you manage a manufacturing company, 2026 probably did not start very calmly for you. The pressure on efficiency is higher than ever before. Energy prices are no longer the shock they were two years ago, but geopolitical uncertainty, trade measures, and tensions in global markets are making planning increasingly difficult. At the same time, the responsibility for results still rests on you.

In such an environment, it may seem that the best strategy is to wait. To be conservative. Not to invest. However, it is precisely in times of uncertainty that it becomes clear who will maintain competitiveness and who will begin to fall behind. If you want to know which Industry 4.0 trends will bring real value in 2026 and which are just marketing noise, read on.

Kľúčové trendy v Industry 4.0 – Čo očakávať v roku 2026? | Key Trends in Industry 4.0 – What to Expect in 2026?

Why Is Tracking Industry 4.0 Trends Especially Important Today?

Companies that follow modern trends and the real possibilities of their application do not operate more efficiently because they want to appear “innovative.” They operate more efficiently because they can identify opportunities earlier where time can be saved, costs reduced, or performance increased—without immediately having to invest in new machines or expand production capacity.

An example is the use of artificial intelligence in procurement processes. Today, systems can easily contact 15 suppliers, summarize price offers, and prepare a comparison. What once took a person days can now be completed by a system within hours.

Without monitoring trends, you would arrive at such efficiency improvements five years later, most likely at a time when it has already become the market standard and you are simply catching up. And this is not some futuristic scenario. It is a practical acceleration of processes that reduces administrative burden and frees up people’s capacity for more valuable tasks.

A very similar situation can be seen in manufacturing digitalization. Companies that build a solid data foundation will be able to respond more quickly to market fluctuations, optimize capacities, and make decisions with lower risk. On the other hand, those that follow trends only passively will be implementing in a few years what their competitors are already using as a standard today.

What Challenges Will Companies Face in 2026?

1️⃣ Geopolitical Uncertainty and Difficult Predictability

The year 2026 is characterized by a high level of unpredictability. Threats of trade restrictions, sudden tariff changes, and tensions between global players can have an immediate impact on supply chains, input costs, and material availability. In a highly globalized environment, a single geopolitical decision can affect the entire market.

For many companies, success may simply mean maintaining the status quo. Not in the sense of stagnation, but in terms of stability. Maintaining margins, performance, and delivery reliability despite external shocks. And it is precisely the companies that have a clear overview of their capacities, efficiency, energy consumption, and bottlenecks that can respond to market fluctuations without panic.

2️⃣ Pressure for Flexibility and Rapid Adaptation

In the past, it was possible to plan production months in advance. Today, the situation is different. Orders fluctuate, customers change priorities, delivery times are shortening, and input prices can change practically overnight. What was true last quarter may no longer apply today. Companies therefore need to be prepared to quickly adjust production capacity, redirect production, or optimize costs.

Such flexibility, however, does not emerge from improvisation. It emerges when you have a clear overview of the real utilization of machines, where downtime occurs, and where hidden reserves exist. A company without data reacts reactively, solving problems only after they arise. A data-driven company, on the other hand, can act preventively, before the problem affects results.

3️⃣ ESG, Energy Efficiency, and Regulation

ESG is no longer just a topic for large multinational corporations. Increasingly, it also affects medium-sized manufacturing companies, either directly through legislation or indirectly through the requirements of customers and partners. If a company wants to comply with standards such as ISO 50001, it must be able to systematically monitor energy consumption at the level of individual devices, evaluate energy efficiency, implement specific measures, and demonstrate their benefits.

In 2026, however, ESG is not just a “reputational” topic. Energy represents a significant cost component. Yet many companies still cannot say exactly which machine consumes the most energy, where unnecessary peaks occur, or what the relationship is between production performance and energy consumption. Without this data, energy management is only an estimate. A company that does not have energy under control also does not have a significant part of its margin under control.

What Risks Do Companies Face If They Neglect Innovation?

A company that changes nothing today may feel stable. After all, machines are running, people are working, and orders are being fulfilled. At first glance, nothing dramatic seems to be happening. The problem is that the loss of competitiveness does not happen suddenly, but gradually. First, costs increase by a few percent. Then delivery times become longer. Later, margins decrease. Eventually, it becomes clear that competitors can produce cheaper, faster, or more flexibly.

Companies that fail to innovate systematically therefore risk:

❌ Greater risk, because in times of crisis, reserves are often what determine survival.
❌ Low ability to respond to market fluctuations, where improvisation replaces real adaptation.
❌ Higher invisible losses, as operating costs increase without companies even realizing it.

One thing is important, however: It is never too late to start. Not all innovations require major investments. Often, it is about systematic work with data, identifying hidden reserves, and gradually improving processes. And perhaps in times of an unpredictable market, focusing on efficiency improvements is wiser than waiting for “a better time.” Because a data-driven company handles uncertainty much more calmly.

Key Industry 4.0 Trends in 2026

👉 1. Automated Data Collection

Manually recording data on paper or in Excel should no longer be the norm today. Digitalization is not new, nor is it rocket science. It is the foundation of efficient management. If a company has not started yet, in 2026 it is high time to map processes, define priorities, and most importantly appoint an internal digitalization ambassador.

👉 2. OEE (Overall Equipment Effectiveness)

If digitalization is the foundation, OEE is the next logical step. The OEE indicator can reveal hidden reserves of 20–30%. And honestly, no AI will deliver such an immediate impact. However, beware of a common misconception: the fact that your machine shows OEE on its display does not mean you are digitalized. If these data remain isolated and are not connected to reporting, you are still operating “on paper.”

👉 3. Energy Efficiency Through EMS and BMS Systems

Energy management is no longer just a “nice to have.” Systems such as EMS and BMS allow companies to monitor consumption at the level of individual machines, optimize operations based on tariffs, identify inefficient equipment, and also prepare operations for ISO 50001.

👉 4. Transition from Reactive to Predictive Maintenance

Reactive maintenance (“we fix it when it breaks”) is today a costly luxury. Transitioning to predictive maintenance means collecting operational data, analyzing trends, and most importantly planning interventions before a failure occurs. Combined with a CMMS system, this creates a managed maintenance ecosystem that reduces downtime, emergency interventions, and the secondary damage associated with them.

👉 5. Unified Platforms (Ignition)

There is no need to discard existing systems. However, if a company is starting from scratch, it is wise to choose a platform that can scale. Ignition is an example of a solution that connects all critical systems, enables ETL processes, and simplifies data integration. A unified platform reduces chaos and increases the clarity of data flows.

👉 6. Digital Workforce and High Performance HMI

This topic is discussed far less than it deserves, yet its impact in practice is enormous. The ISA-101 standard defines High Performance HMI principles such as fewer colors, more context, highlighting only critical states—all designed to reduce the cognitive load on operators. A modern interface should not be about 3D graphics and blinking flames, but about the operator making fast and correct decisions.

👉 7. Cybersecurity as an Inherent Part of Projects

The question today is no longer: “Will a company become a target of an attack?” but rather: “When will it become a target?” Cybersecurity therefore must be an inherent part of every project, just as natural as occupational safety, without compromise. Not as a separate add-on, but as a fundamental architectural layer of the solution.

👉 8. Big Data and Advanced Analytics

Big Data only make sense when a company is fully digitalized, the data are reliable, and the processes work properly. At that point, connecting data with AI can bring an additional 2–3% optimization. However, as we described in the article “How Big Data Helps Reduce Costs and Boost Performance in Manufacturing Enterprises“, advanced analytics is an extension, not a replacement for fundamental digitalization.

👉 9. AI as a Tool, Not a Goal

Artificial intelligence is currently experiencing enormous hype, perhaps even greater than Big Data once did. It is clear that AI is here to stay and will have its place in industry. However, at the moment it is often overestimated and applied in situations where it does not deliver real value.

Companies should not start with the question “How do we implement AI?”, but rather “What problem do we want to solve?”. And the solution does not automatically have to be artificial intelligence. Often, automated data collection and basic process digitalization are enough. The real value lies in the correct and justified use of technology, not in the technology itself.

How to Prepare for These Trends?

If digitalization or innovation is to be successful, it cannot be random or driven only by current trends. It requires a clear structure, realistic expectations, and a process that minimizes risk while maximizing benefits. A properly designed approach also ensures that the investment will not become a one-time project, but rather a long-term tool for optimization.

A proven approach therefore looks as follows:

  • 1️⃣ Audit and process mapping
  • 2️⃣ Identification of priorities and benefits
  • 3️⃣ Solution design
  • 4️⃣ PoC (Proof of Concept)
  • 5️⃣ Implementation
  • 6️⃣ Long-term monitoring and optimization

When deciding on innovations, the greatest challenge is often to objectively evaluate one’s own processes. Internal teams are naturally immersed in daily operations, and many inefficiencies gradually become the “norm” that no one questions anymore. That is why it is beneficial to involve an external partner with practical experience, who can bring an independent perspective, reduce the risk of incorrect decisions, and accelerate the path to measurable results.

Even 2026 Cannot Stop Progress

Market uncertainty should not be a reason for stagnation. On the contrary, it is an impulse to focus on areas that increase flexibility and efficiency. Digital transformation is not a trend for show. It is a tool that enables companies to respond to unexpected situations faster than their competitors. If you want to find out where the greatest potential lies within your production, let’s start with a non-binding consultation.

“We may not know what global politics will bring. We may not know how markets will evolve. But one thing is certain. The world will not stop. Companies may decide to be more conservative, yet there is still room for innovations that deliver real value.” – Matej Medvecký, Founder & Technical Lead, IoT Industries Slovakia

Why Choose IoT/IIoT Implementation with IoT Industries?

Traditional companies typically specialize in OT (operational technologies, such as production lines and devices) or classic enterprise IT systems. However, we are able to connect both of these worlds. Our unique expertise in integrating OT and IT allows us to deliver innovative solutions in digital transformation, enhancing efficiency, reliability, and competitiveness for manufacturing companies.
ISA-101 – Štandard pre moderné a prehľadné HMI rozhrania | ISA-101 – Standard for Modern and Clear HMI Interfaces

ISA-101 – The Standard for Modern, High-Performance HMI Interfaces

Many manufacturing companies invest heavily in modern technologies, yet the interfaces people work with every day often lag behind. Screens are inconsistent, each one looks different, colors have no clear meaning, and critical information gets lost in a sea of details. The result is higher error rates, lower safety, and unnecessary cognitive load for operators. The ISA-101 standard was created as a response to these issues. It provides clear guidelines for how industrial displays should be designed so they are understandable, easy to read, and help people in manufacturing make the right decisions at the right time.

ISA-101 – Štandard pre moderné a prehľadné HMI rozhrania | ISA-101 – Standard for Modern and Clear HMI Interfaces

What is ISA-101?

ISA-101 is an international standard that defines how human–machine interfaces, known as HMI (Human-Machine Interface), should be designed. These are the screens through which operators monitor production status, control technological processes, and respond to faults. In practice, ISA-101 represents a set of principles and recommendations for a consistent and understandable visual “language” that allows operators to immediately recognize what is operating normally and what is not.

Think of it like road signage. No matter where you drive or what car you use, traffic signs have the same meaning everywhere, so drivers don’t have to think about what they mean. ISA-101 works in the same way—just for industrial screens.

The goal of ISA-101 is to reduce clutter and chaos on screens. Instead of excessive colors, icons, and animations, it relies on simple and clear visualizations where every color or highlight has a clearly defined meaning. When something goes wrong, the problem immediately stands out and cannot be overlooked. In other words, ISA-101 helps people make fewer mistakes and respond faster.

The acronym ISA stands for the International Society of Automation, the organization that develops these standards. The number 101 refers to the specific standard focused on HMI design.

An important milestone is that ISA-101 has recently been adopted as the international standard IEC 63303. This officially places its principles among recognized standards used across industries worldwide. For companies, this provides confidence that ISA-101 is not a “trend” or a subjective design approach, but a practice-proven standard backed by international standardization.

Why was the ISA-101 standard created?

The ISA-101 standard emerged from real-world experience in manufacturing plants. In practice, it repeatedly became clear how inconsistent and cluttered screens lead to errors, delays, and unnecessary stress in production. The problem was often not the technology itself or a lack of data, but the way data was presented to the people who worked with it every day.

Each screen looked different, colors had different meanings, and operators had to learn how to “read” each machine separately. Visual chaos—too many colors, icons, and animations—meant that everything on the screen appeared equally important. When a real deviation or issue occurred, it could easily get lost among other information.

ISA-101 was created as a response to these situations. It introduced clear rules for how information should be displayed so that it can be understood at a glance. The goal was not to create “prettier HMIs,” but interfaces that reduce mental load, shorten reaction time, and help people make the right decisions—even under pressure.

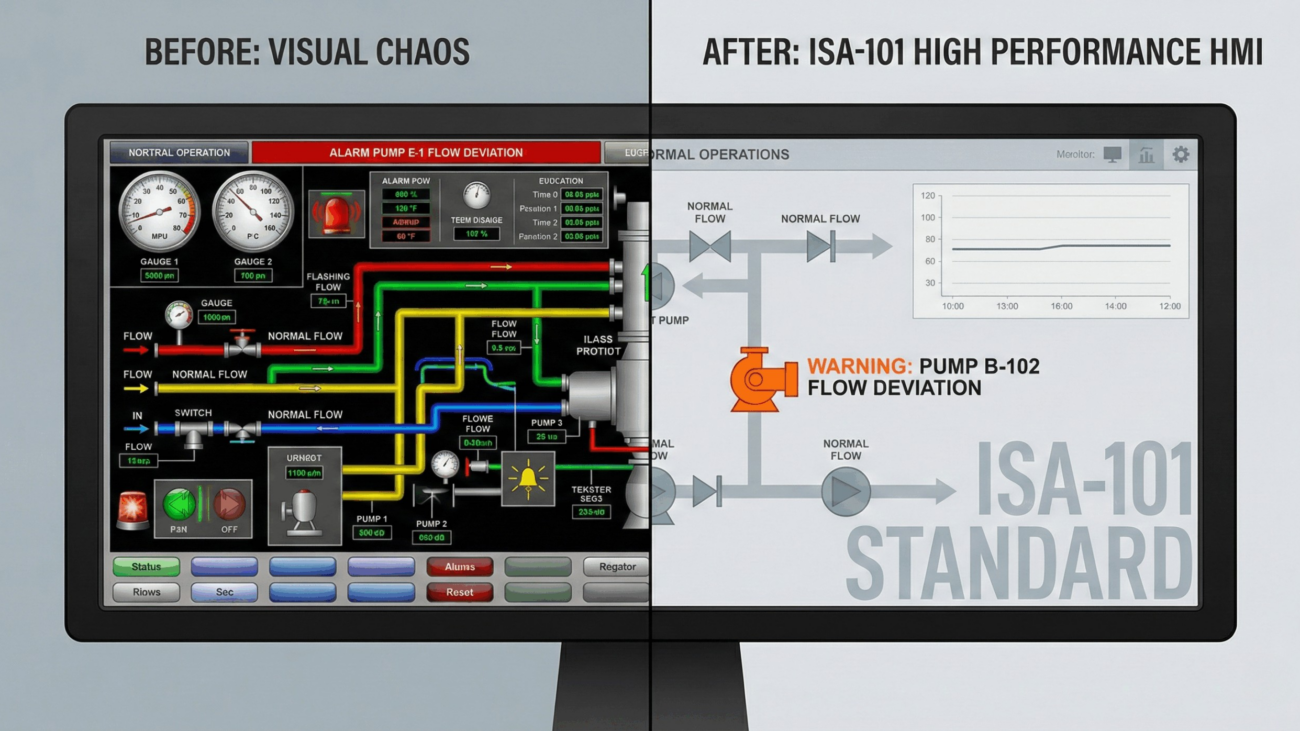
Traditional HMI approachesISA-101
Many colorsMinimalist, meaning-based colors
AnimationsSimple, clear elements
ChaosConsistent structure
Reactive problem handlingPrevention and fast situational awareness
HMI Before
HMI After

The High Performance HMI Principle

One of the key pillars of the ISA-101 standard is the High Performance HMI principle. It is based on a simple but often overlooked fact: the human brain has a limited capacity to process large amounts of visual information at once.

High Performance HMI therefore changes the way we think about HMI design. The goal is no longer “to display everything”, but to display what truly matters, in the right way. The normal operating state of a process should be visually calm and unobtrusive, so operators do not have to constantly monitor every detail. In contrast, deviations, faults, or risky conditions must be clearly and immediately recognizable, without searching or overthinking.

A crucial role in this approach is played by ISA-101 color usage. In High Performance HMI, colors are not decorative—they are signals. Gray and neutral tones represent the normal state, while yellow and orange indicate warnings and deviations. Red is reserved exclusively for critical conditions. This ensures that each color has a clear and consistent meaning.

ISA-101 also takes into account a real-world factor that is often overlooked in practice: color blindness. Approximately 8% of men suffer from some form of color vision deficiency, which means such operators are commonly present in manufacturing environments. For this reason, ISA-101 does not rely on color alone to convey meaning. Critical states and alarms are also supported by shapes, symbols, and clear visual elements, ensuring information is understandable to everyone, regardless of their ability to distinguish colors.

Equally important is the hierarchy of information. High Performance HMI works with multiple screen levels—from high-level overview screens down to detailed views of individual devices. The operator first sees where a problem is occurring, then what is causing it, and only then how to resolve it. The interface guides the user logically and systematically, instead of overwhelming them with information.

What Are the Practical Benefits of ISA-101?

The result of applying ISA-101 is an HMI that supports so-called situational awareness—the ability to quickly understand the current state of production, its development, and potential risks. Operators are not forced to constantly “read the screen”, but react only when necessary. This reduces mental load, shortens reaction time, and significantly minimizes the likelihood of human error.

From a business perspective, ISA-101 High Performance HMI also delivers long-term benefits. New employees can be trained faster, operator substitution between production lines becomes easier, and technology changes can be implemented without introducing visual chaos. The HMI thus becomes a stable and reliable tool that grows together with the production system.

Companies that modernize their HMI according to ISA-101 gain:

  • faster operator response times,
  • lower error rates,
  • higher safety,
  • better use of production data,
  • readiness for the next steps of digital transformation.

Where to Get the ISA-101 Download?

The official ISA-101 download is available on the ISA organization’s website. It is a paid document that includes detailed HMI design rules, recommended practices, screen examples, terminology, and methodology. For serious projects, working with the official documentation is essential—especially if the goal is long-term sustainability of the solution.

How Does ISA-101 Fit into Industry 4.0?

Industry 4.0 brings enormous amounts of data into manufacturing. However, data alone is not enough. If people cannot see it in a clear and understandable form, it remains just numbers hidden in systems that are not effectively used in practice.

This is where ISA-101 plays a critical role, because it ensures that information from SCADA, MES, OEE, EMS, and other systems is presented in a way that operators and management can immediately understand. Thanks to a consistent and clear HMI, data from digital manufacturing is transformed into fast decisions and concrete actions, not just additional reports.

At IoT Industries, we therefore do not see ISA-101 as a standalone “HMI topic”, but as a natural part of digital transformation and Industry 4.0. When designing solutions, we focus on ensuring that screens are not only technically correct, but also readable, consistent, and usable in real operational conditions. The result is a production environment where technology, data, and people work together as one.

A Comprehensive, Tailor-Made Solution from IoT Industries

At IoT Industries, we do not approach ISA-101 only from an implementation perspective. We are also actively involved in its development as members of the ISA-101 committee, which contributes directly to the creation and evolution of this standard. This means that we understand exactly why individual principles were created, how they should be applied correctly, and where the standard is heading next.

Thanks to the combination of international standards, real-world operational experience, and active participation in their development, we are able to design HMI interfaces that are not just “compliant with the standard,” but truly effective in everyday manufacturing operations. If you want to elevate your HMI interfaces to a professional level and prepare your production for the future, get in touch with us. We’ll be happy to show you how ISA-101 works in practice.

Why Choose IoT/IIoT Implementation with IoT Industries?

Traditional companies typically specialize in OT (operational technologies, such as production lines and devices) or classic enterprise IT systems. However, we are able to connect both of these worlds. Our unique expertise in integrating OT and IT allows us to deliver innovative solutions in digital transformation, enhancing efficiency, reliability, and competitiveness for manufacturing companies.